

Chuanyi Water Treatment Supports Full Operation of Zhangqiu Clean Energy Cogeneration Project
Share this Post
High-Purity Water Empowers Green Heating | CHUAN YI
Recently, the Shutdown & Heat Source Replacement Project for Coal-fired Power Units of Jinan Energy Xinsheng Cogeneration has been fully completed and commissioned. As a key clean energy upgrading initiative in Zhangqiu District, the project has phased out outdated coal-fired cogeneration units and built a brand-new dual-energy heat supply plant, kicking off a new era of eco-friendly industrial heating across the region.
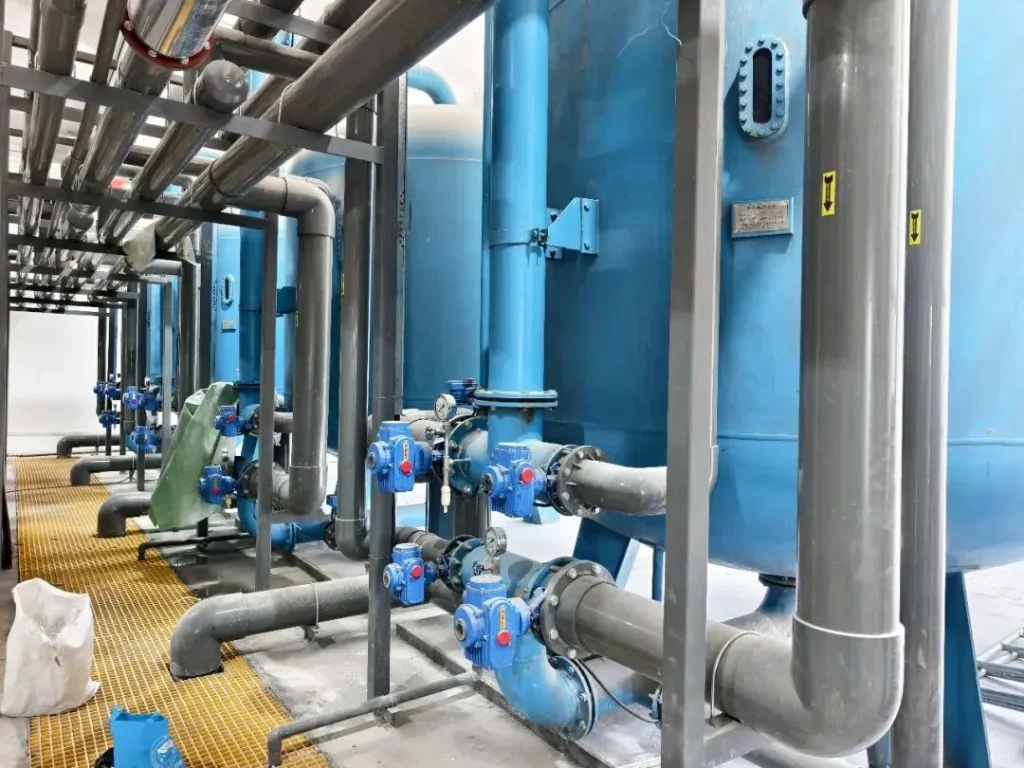
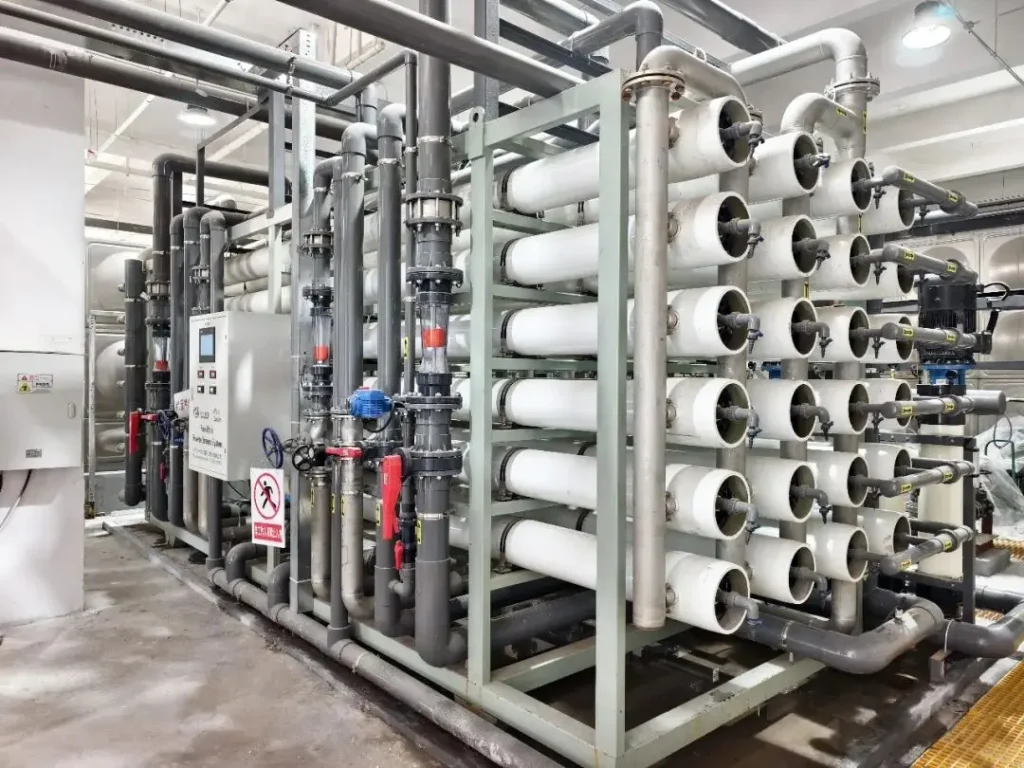
Throughout project construction, Chuanyi Water Treatment provided full-cycle support for the supporting environmental water system. We customized and delivered a set of 2×70 ton/hour Reverse Osmosis (RO) water treatment equipment. Featuring high standard, stable performance and intelligent control, our tailor-made industrial water solution lays a solid core foundation for steady steam generation, long-term operation and environmental compliance of the clean energy heat plant, serving as an essential auxiliary for this green heating upgrade project.
Developed by Jinan Heli New Energy Co., Ltd., an affiliate under Jinan Energy Group, the project actively responds to national coal-fired unit phase-out and dual-carbon decarbonization policies. It retires coal-fired thermal power facilities in service for nearly 30 years and builds an innovative dual-clean-energy heating system dominated by biomass with natural gas as peak-shaving backup, exclusively supplying industrial steam for local manufacturers and realizing a complete green transformation from conventional coal-fired heating.
For cogeneration plants, boiler feed water quality directly impacts unit operating efficiency, service life and operational safety, making water treatment equipment an indispensable core facility and the “hidden heart” sustaining long-term stable plant operation. Our custom-built 2×70T/h RO system is precisely engineered to cope with the plant’s large-volume, high-load and non-stop production conditions, fully meeting operational standards of dual-fuel boilers.
✅ 1. Secure Uninterrupted Production & Eliminate Steam Cutoff Risks
All 26 food, biotech and new-material manufacturers operate non-stop production lines with strict requirements for steady steam supply. Our modular redundant-designed 2×70T/h RO system enables round-the-clock stable operation with constant effluent quality and sufficient water output, matching instant grid-connected steam switching requirements of the plant. It avoids boiler breakdown and unplanned shutdown triggered by substandard feed water, securing continuous manufacturing for all downstream industrial clients.
✅ 2. Reduce Operating Costs & Extend Equipment Service Life
Unprocessed raw water causes severe boiler scaling, dropping thermal efficiency, boosting power consumption and accelerating equipment deterioration with soaring maintenance expenses. The RO system deeply purifies source water to lower water hardness and ionic content, drastically mitigating scaling and pipeline corrosion, improving boiler heat exchange efficiency and cutting energy waste. It extends the service lifespan of boilers and piping while trimming long-term repair and replacement costs to deliver remarkable economic benefits.
✅ 3. Low-carbon Green Design Aligned with Environmental Standards
Focused on phasing out coal-fired heating to advance decarbonization, the project follows local eco-friendly development plans. Adopting physical membrane filtration without frequent acid-alkali chemical regeneration, Chuanyi’s RO equipment slashes chemical consumption and waste discharge compared with traditional water treatment processes. Its low-carbon, pollution-free feature fits perfectly with the plant’s clean-energy positioning and facilitates the fulfillment of national dual-carbon targets with better environmental indicators than outdated coal-fired facilities.
✅ 4. Intelligent Control for Large-scale Plant Management
Fitted with an intelligent monitoring system, the equipment tracks real-time operating data including water pressure, flow rate, water quality and membrane performance with automatic startup/shutdown and early fault alert functions. Minimal manual intervention is required to streamline daily management, ideal for standardized, intelligent large-scale plant operation and improved overall system efficiency.